Add: NYaqian Road No128 Yaqian Town Xiaoshan Hangzhou Zhe Jiang China.
Tel: 0086-0571-82602080
Fax: 0086-0571- 82758132
E-mail: [email protected]
Article Directory
That gap is not a production defect. It is a specification outcome. Blanket yarn behavior is set by a bundle of interdependent numbers, and filament count is merely the one that is easiest to feel. The same logic runs through loft, color depth, pilling, and how a blanket looks after thirty domestic washes.
Read a blanket yarn specification and you are reading a set of trade-offs. Push one parameter toward softness and another moves toward pilling. The sections below work through what each parameter does, where the practical limits sit, and which values belong in a purchase order.
Softness in a blanket is controlled primarily by denier per filament, or dpf. At a constant 300 denier total, moving from 96 filaments at 3.13 dpf to 576 filaments at 0.52 dpf cuts the bending stiffness of each individual filament by roughly 97 percent.
The mechanism is geometric. Filament diameter scales with the square root of dpf, and the force needed to bend a filament scales with the fourth power of that diameter, so bending stiffness tracks dpf squared. Halve the dpf and a filament becomes four times easier to bend; move from 3.13 to 0.52 dpf and the change reaches a factor of 36.
Finer filaments pack more surface area and finer air channels into the same yarn cross-section, which is why a 0.52 dpf blanket traps more still air per gram than a 3.13 dpf blanket of the same weight. The trade-off is mechanical: as dpf falls, resistance to flex fatigue falls with it, and pilling risk climbs unless tenacity is held at 3.5 cN/dtex or above.
 Blanket Yarns ManufacturersProduct Specifications Technical ParametersView Product →
Luster, cover, and color depth are decided before a blanket reaches the finishing line. Four yarn parameters control how the finished product reads under light: cross-section shape, delustrant content, interlace level, and dyeing route.
| Specification | Typical options | Effect on the finished blanket |
|---|---|---|
| Cross-section | Round, trilobal, hollow | Round sections scatter light and read matte; trilobal sections return more light and lift luster; hollow sections add bulk at lower fabric weight |
| Delustrant, titanium dioxide | Bright near 0.03 percent, semi-dull near 0.3 percent, full dull near 2 percent | Higher delustrant content removes glare and produces the wool-like matte surface that hides soil |
| Interlace | NIM at near zero nodes per meter, SIM near 40, HIM at 60 or more | Low interlace opens the pile and can look uneven; high interlace tightens the yarn and reduces loft |
| Crimp contraction | 3 to 6 percent, measured to ASTM D4031 | More crimp builds cover and a softer visual texture; excess crimp produces a pebbled surface |
| Color route | Package-dyed or dope-dyed, also called solution-dyed | Solution-dyed yarn holds ISO 105-C06 grade 4 to 5 through washing and removes lot-to-lot shade drift |
Shade drift is the appearance failure that appears last and costs the most. A package-dyed lot can move half a grade between dye batches, and the shift becomes obvious when two blankets from different batches are laid side by side. Solution-dyed yarn carries pigment inside the polymer, so lot-to-lot color difference is normally held within a Delta E of 1.0.
Luster is a lighting decision, not a quality grade. A trilobal bright yarn specified for a display under warm 3,000 K lighting can look synthetic, while the same yarn reads as premium under cooler showroom light. Match cross-section to the light where the blanket will be sold.
 Polyester DTY Yarns SuppliersProduct Specifications Technical ParametersView Product →
A blanket yarn that meets ISO 2060 for linear density, ISO 2062 for tensile properties, and ASTM D4031 for bulk will hold pile height, resist pilling, and keep its dimensions through repeated washing. All three are yarn-stage measurements, so they can be verified before a single blanket is knitted.
| Property | Test method | Typical blanket yarn target |
|---|---|---|
| Linear density | ISO 2060 | Within 2 percent of nominal denier |
| Tenacity and elongation | ISO 2062 or ASTM D2256 | 3.5 to 4.2 cN/dtex, elongation 20 to 30 percent |
| Bulk and crimp | ASTM D4031 | Crimp contraction between 3 and 6 percent |
| Boiling-water shrinkage | 30 minutes at 95 to 100 degrees Celsius | Under 4 percent, under 2 percent for low-shrink grades |
| Abrasion | ISO 12947-2 Martindale | No breakdown after 25,000 rubs at 12 kPa |
| Pilling | ASTM D4970 | Grade 4 or better after 2,000 rubs |
| Color fastness to washing | ISO 105-C06 | Grade 4 minimum, grade 4 to 5 when solution-dyed |
| Formaldehyde content | Oeko-Tex Standard 100 | 16 mg/kg for Class I baby blankets, 75 mg/kg for Class II |
The conflict rarely shows up as abrasion failure. It shows up as pilling, because fine filaments with low flex life migrate to the surface and form fuzz balls long before the pile wears through. Moving from 0.5 dpf to 1.2 dpf typically raises Martindale pilling performance by a full grade while costing a measurable amount of initial softness.
Where a blanket has to carry a functional claim on the label, such as antibacterial protection for healthcare textiles or antistatic behavior for bedding in dry climates, the additive or blend carries the property and the dpf range has to be retested for pilling before the specification is frozen.
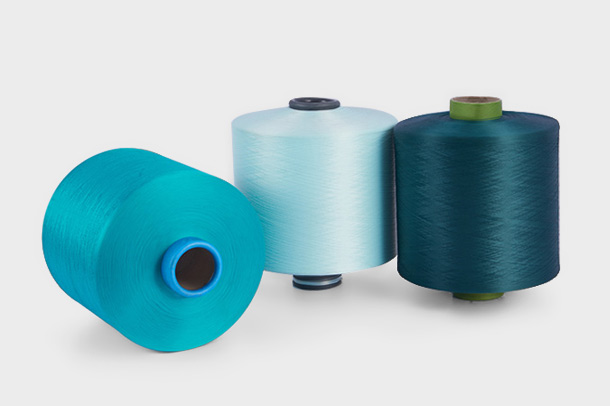 Functional Yarn ManufacturersPerformance Integration at the Yarn Stage: Functional properties engineered into the yarn — through polymer modification, fiber cross-section design, or additive incor...View Product →
Build the specification backwards from the finished blanket. Fix fabric weight and machine gauge first, then work through filament architecture, crimp, shrinkage, and color.
Most blanket quality disputes trace back to parameters that were never written down rather than to defective yarn. Linear density and color are habitually specified; oil pick-up, interlace, shrinkage, and lot tolerance usually are not.
Oil pick-up is the clearest example of a missing number. Yarn delivered at 0.4 percent finish runs tight and generates static on a high-speed knitter, while yarn at 2.0 percent feels greasy and can stain pale blankets. A written band of 0.8 to 1.5 percent prevents both failures at no cost.
Before fixing numbers with a new supplier, confirm how the yarn is spun, textured, and heat-set. Zhejiang Hengyuan Chemical Fiber Group Co., Ltd. sets out its manufacturing structure and its research and development center on the same site, which is where texturing and heat-setting parameters are normally controlled.
A blanket yarn specification is only enforceable when the test method is named. Tenacity means nothing without ISO 2062 or ASTM D2256, and shrinkage means nothing without a stated temperature and dwell time.
Between 0.5 and 1.0 dpf. Below 0.9 dpf the filament qualifies as microfibre under the CIRFS definition, and tenacity then has to stay at 3.5 cN/dtex or above to keep pilling at ASTM D4970 grade 4.
No. Above roughly 576 filaments at 300 denier, softness gains flatten while spinning cost, tension sensitivity, and pilling risk keep climbing. The practical ceiling for most blanket programs sits at 0.5 dpf.
Test three production lots against ISO 2060, ISO 2062, and ASTM D4031, then knit a 1 kilogram sample blanket and wash it five times at 40 degrees Celsius. Pile height loss above 5 percent usually signals a shrinkage or crimp problem.
Yes, inside a defined window: 1.0 to 1.5 dpf, tenacity at 3.8 cN/dtex or higher, crimp contraction of 3 to 5 percent, and boiling-water shrinkage under 2 percent.
Zhejiang Hengyuan Chemical Fiber Group Co.,Ltd. is a professional China polyester filament yarns manufacturers and polyester color yarn suppliers, Established in 2006 ,located in YaQianTown Xiaoshan Hangzhou – One of the Center of polyester yarn Industry in China.
Products
Contact info
Copyright © Zhejiang Hengyuan Chemical Fiber Group Co.,Ltd. All rights reserved